EU PPWR Grade-A (>95% Mono-PE) · EN 13432 & How2Recycle · MOQ FROM 500 PCS ($0 DIGITAL PLATE)
100% Recyclable Mono-Material PE (BOPE / EVOH-PE), GRS PCR & EN 13432 Compostable Pouches
FlexPouchMFG™ engineers circular flexible packaging compliant with the 2026 European Packaging and Packaging Waste Regulation (EU PPWR), UK Plastic Packaging Tax, and US How2Recycle® store drop-off guidelines. Our high-barrier Mono-PE laminates combine biaxially oriented polyethylene (BOPE 25μm) with a 5-to-9 layer co-extruded EVOH-PE sealant (<4.6% EVOH by weight, >95.4% PE), delivering OTR < 0.85 cm³/m²·24h, All-PE zippers, and All-PE degassing valves without PET or aluminum foil.
"The biggest challenge when switching from PET/PE to 100% Mono-PE pouches is heat-seal window collapse: standard outer PE melts at 118°C while the inner PE seals at 112°C, causing severe seal-jaw sticking and gusset shrinking on existing bag-making and filling lines. We solve this by pairing a cross-direction-oriented high-density BOPE outer skin (heat-resistant to 142°C) with a plastomer-modified inner skin that seals cleanly at 98°C—giving you a 44°C operating window."
MULTI-LAYER BARRIER LAMINATE ARCHITECTURE · NORDMECCANICA SOLVENTLESS
FP-MPE-130 EU PPWR Grade-A Mono-PE Structure (130 μm) — Micron Cross-Section & Functional Layer Breakdown
VERIFIED LAMINATE STRUCTURES, MICRON TOLERANCES & 2026 FOB MATRIX
1. Custom Laminate Structures, Micron Tolerances & Reference FOB Matrix
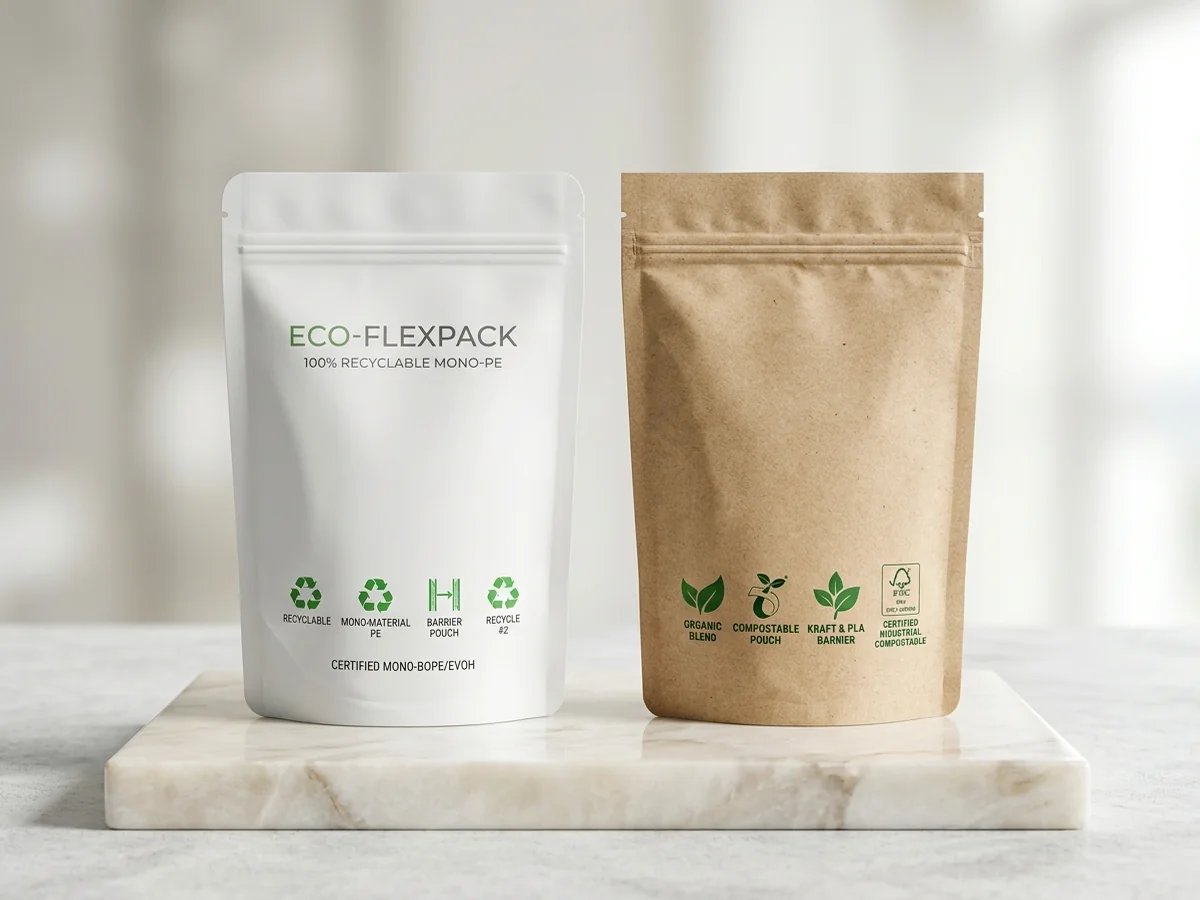
Multi-material laminates containing PET, Nylon, or Aluminum bonded to Polyethylene are classified as non-recyclable under 2026–2030 EU PPWR eco-modulation fee schedules and California SB 54. We help food, coffee, pet nutrition, and clean-beauty brands transition seamlessly to three verified sustainable platforms: (1) 100% Recyclable Mono-PE/Mono-PP (RIC #4 / #5), (2) GRS-Certified 30%–50% Post-Consumer Recycled (PCR) pouches, and (3) TUV-certified EN 13432 / ASTM D6400 Compostable Kraft/NatureFlex™/PBAT+PLA pouches.
| Eco Platform SKU | Sustainable Film Architecture (μm) | Recyclability / Compost Spec | OTR / WVTR Barrier | Ideal Brand Application | Factory FOB (USD/pc) |
|---|---|---|---|---|---|
| PM-EC-601 (Mono-PE High Barrier) | Matte BOPE 25 / AlOx-Coated MDO-PE 20 / EVOH-PE 75 | 96.2% PE (RecyClass Grade A · #4 LDPE) | <0.85 cc / <1.20 g | Roasted Coffee (+ PE Valve), Nuts, Pet Treats, Bath Salts | $0.068 – $0.195 |
| PM-EC-602 (Mono-PE Std Barrier) | Gloss/Matte BOPE 25 / Metallocene LLDPE 85 + PE Zip | 98.5% Mono-PE (How2Recycle Store Drop-Off) | <280 cc / <2.10 g | Frozen Foods, Dry Grains, Cotton Pads, Apparel & Refills | $0.052 – $0.135 |
| PM-EC-603 (Mono-PP Retort/Hot) | BOPP 20 / AlOx-BOPP 18 / High-Clarity CPP 70 | 97.8% Mono-PP (RIC #5 Polypropylene Stream) | <0.90 cc / <0.80 g | Hot-Fill Snacks, Baked Goods, Mediterranean Olives, Spices | $0.058 – $0.148 |
| PM-EC-604 (GRS 35% PCR Pouch) | PET 12 / VMPET 12 / 50%-PCR Co-Ex LLDPE 75 | 35.4% Total Post-Consumer Recycled Plastic | <0.75 cc / <0.95 g | UK Plastic Tax Exempt (>30% PCR) Cosmetics & Supplements | $0.056 – $0.142 |
| PM-EC-605 (TUV Compostable) | FSC Kraft 45g / Futamura NatureFlex™ NK 23 / PBAT+PLA 60 | EN 13432 & ASTM D6400 (>90% Biodegrade in 180d) | <2.20 cc / <4.50 g | Organic Tea, Botanical Powders, Zero-Waste Soap & Superfoods | $0.095 – $0.275 |
INTERACTIVE ENGINEERING SPECIFICATIONS & QA PROTOCOLS (CLICK TO EXPAND)
Benchtop-to-Plant Laminate SOP, MOCON Cpk Tolerances, Competitor Cross-Reference & Line Troubleshooting
Module I & II — 1,000g Batch Adhesive Stoichiometry, 52°C Curing SOP & MOCON / Agilent QC Tolerances (Cpk ≥ 1.67) EXPANDED LAB SOP
Mono-PE and compostable laminates are highly sensitive to web stretching under tension; we run low-tension servo-driven Nordmeccanica lines with recycle-ready polyurethane adhesives.
Ratio: Henkel Loctite Liofol Recycle-Ready solventless adhesive mixed at 100 : 55 (certified by RecyClass and Cyclos-HTP not to discolor recycled PE pellets).
Temp & Viscosity: Low-temperature nip at 38°C ± 1°C to prevent BOPE/MDO-PE thermal relaxation; viscosity maintained at 840 mPa·s.
Coating Weight: 1.50 g/m² ultra-thin coat weight keeping non-polyolefin adhesive fraction strictly below 1.4% of total pouch mass (±0.12 g/m² beta-gauge).
Tension: BOPE 25μm unwind tension held strictly at 65 N (55% lower than PET tension) with closed-loop ultrasonic roll diameter calculation.
Curing Profile: 40°C ± 1°C for 48 hours (low-temperature curing prevents PBAT/PLA crystallization embrittlement and BOPE shrink)
Target Peel Bond: ≥ 3.5 N/15mm on Mono-PE; ≥ 2.6 N/15mm (or fiber tear) on FSC Kraft / NatureFlex™ / PBAT+PLA compostable structures (ASTM D903).
OTR: ≤ 0.85 cm³/(m²·24h) at 23°C, 50% RH for AlOx-MDO-PE + EVOH-PE; ≤ 2.20 cc for metallized NatureFlex™ cellulose compostable laminates.
WVTR: ≤ 1.20 g/(m²·24h) for high-density MDO-PE/BOPE moisture barrier structures.
GC Solvent: Zero fluorinated PFAS, zero PVDC (chlorine-free), zero BPA/Phthalates; heavy metals Pb+Cd+Hg+Cr(VI) < 15 ppm (limit <100 ppm per EN 13432).
Heat-Seal, Hot-Tack & Drop Integrity: 36.0 to 48.0 N/15mm using ultrasonic pre-tacking and impulse-cooled jaws to yield wrinkle-free flat seams on Mono-PE. · Burst & Drop: 5-drop 1.2m survival at 23°C and 0°C; compostable PBAT+PLA pouches include batch elongation-at-break testing (>280%) to guarantee zero brittle shelf cracking. (Every sustainable pouch lot is accompanied by a polymer mass-balance breakdown sheet verifying exact PE/PP/EVOH weight percentages for EPR fee filings.)
Module III — International Competitor 1:1 Cross-Reference Matrix (Amcor / Mondi / Berry / Constantia Parity) SAVE 38%–52% BOM
| Global Reference Brand / Series | FlexPouchMFG™ 1:1 Code | Matched Multi-Layer Construction | Barrier & Sealing Parity | Commercial Advantage |
|---|---|---|---|---|
| Amcor® AmPrima® PE Plus | PM-EC-601 | BOPE25 / AlOx-MDO-PE20 / EVOH-PE75 | Identical >95% PE RecyClass Grade-A & <1.0 cc OTR | 44% lower FOB; MOQ 500 digital pilot runs |
| Mondi® EcoSolutions Mono-Formable | PM-EC-602 | BOPE25 / mLLDPE85 + All-PE Pocket Zipper | 100% drop-in replacement for PET/PE on HFFS lines | Includes heat-resistant matte lacquer up to 145°C |
| Tipa® / Elevate® Compostable Stand-Up | PM-EC-605 | FSC Kraft 45g / NatureFlex™ 23 / PBAT+PLA 60 | Certified EN 13432 / ASTM D6400 bio-disintegration | Freshly extruded PBAT+PLA with 12-month shelf guarantee |
Module IV & V — Global HS Tariff Codes, FDA/EU/EAEU Migration Limits & 5 Filling-Line Troubleshooting Scenarios 5 LINE FIXES + HS CODES
Audit-ready documentation for European EPR eco-modulation, UK Plastic Packaging Tax exemption, and US state-level EPR laws (CA SB 54, CO, OR). Primary HS Code: 3923.21.00 (100% Mono-Polyethylene recyclable pouches — RIC #4) | Foil-Backed HS Code: 3923.29.10 / 4819.40.00 (Biopolymer PLA/PBAT and FSC Kraft paper compostable bags)
- US FDA & MoCRA: Compliant with US FDA 21 CFR 177.1520 (Virgin & FDA NOL food-grade PCR PE), ASTM D6400 (Compostable), and How2Recycle® Store Drop-Off.
- EU No 10/2011 & PPWR 2026: Designed for EU PPWR 2026 Design-for-Recycling (DfR) Grade A (>95% PE, EVOH <5%, zero carbon-black NIR-detectable pigments) and EN 13432.
- Eurasian EAEU ТР ТС 005/2011: Compliant with ТР ТС 005/2011 loop symbol and polymer identification marking (04 LDPE / 05 PP).
| Failure Mode & Symptom on Filling Line | Root-Cause Material / Mechanical Diagnosis | FlexPouchMFG™ Preventive Laminate & Process Solution |
|---|---|---|
| Scenario 1: Wrinkled, Shrunken, or Melted Outer Gusset Seals When Running Mono-PE on Existing Filling Machines | Standard LDPE outer layers melt at 115°C under the customer's 145°C heat-seal bar. | We apply a cross-linked heat-resistant UV/PU protective topcoat over 5x-stretched high-density BOPE, raising outer jaw stick resistance to 145°C while the inner plastomer seals at 98°C. |
| Scenario 2: Black Mono-PE Pouches Rejected as Non-Recyclable by Optical Sorting Plants in Germany & UK | Traditional Carbon Black ink absorbs Near-Infrared (NIR) laser beams at 1,600–1,750 nm, blinding optical sorters. | We print all dark/black recyclable pouches with Carbon-Free NIR-Reflective Black pigments so MRF optical sorters accurately identify the PE substrate. |
| Scenario 3: Compostable PLA/PBAT Pouches Becoming Brittle or Splitting Along Bottom Seals After 7 Months | Hydrolytic chain scission of polylactic acid (PLA) when exposed to high ambient humidity (>65% RH) and heat. | We blend chain-extender stabilizing masterbatch into freshly blown PBAT/PLA film and pack empty pouches in moisture-proof master liner bags with silica desiccant. |
| Scenario 4: Standard Nylon/PP Coffee Valve Making a Mono-PE Coffee Bag Non-Recyclable | Mixing a Nylon or PP degassing valve onto a PE pouch contaminates the #4 LDPE recycling stream. | We ultrasonic-weld an injection-molded 100% Polyethylene (All-PE) WIPF® W604E degassing valve and All-PE zipper so 100.0% of the pouch components are pure polyethylene. |
| Scenario 5: PCR (Post-Consumer Recycled) Film Showing Gel Specks or Slight Odor in Food/Cosmetic Pouches | Mechanical PCR resin used directly on the food-contact layer. | In PM-EC-604, we encapsulate FDA-NOL deodorized PCR resin strictly inside the middle core of a 3-layer A/B/A co-extrusion while keeping the inner contact skin 100% virgin metallocene PE. |
7. Deep-Dive Polymer Physics & Co-Packer Line Qualification for 100% Recyclable Mono-Material PE (BOPE / EVOH-PE), G
When qualifying 100% Recyclable Mono-Material PE (BOPE / EVOH-PE), GRS PCR & EN 13432 Compostable Pouches across commercial production runs (covering SKUs PM-EC-601 (Mono-PE High Barrier), PM-EC-602 (Mono-PE Std Barrier), PM-EC-603 (Mono-PP Retort/Hot), PM-EC-604 (GRS 35% PCR Pouch), PM-EC-605 (TUV Compostable)), packaging engineers must evaluate the thermo-mechanical interaction between multi-layer constructions (Matte BOPE 25 / AlOx-Coated MDO-PE 20 / EVOH-PE 75 | Gloss/Matte BOPE 25 / Metallocene LLDPE 85 + PE Zip | BOPP 20 / AlOx-BOPP 18 / High-Clarity CPP 70 | PET 12 / VMPET 12 / 50%-PCR Co-Ex LLDPE 75 | FSC Kraft 45g / Futamura NatureFlex™ NK 23 / PBAT+PLA 60) and target filling regimes (Roasted Coffee (+ PE Valve), Nuts, Pet Treats, Bath Salts; Frozen Foods, Dry Grains, Cotton Pads, Apparel & Refills; Hot-Fill Snacks, Baked Goods, Mediterranean Olives, Spices; UK Plastic Tax Exempt (>30% PCR) Cosmetics & Supplements; Organic Tea, Botanical Powders, Zero-Waste Soap & Superfoods). Under high-speed converting on Totani and Karlville pouch lines, differential web elongation between the outer print carrier and the inner sealant must remain below 0.15% to prevent curl, zipper wave, or register drift.
Furthermore, our laboratory validates each lot of 100% Recyclable Mono-PE (BOPE/EVOH-PE) & Home Compostable Pouches against real-world supply chain stressors: high-altitude air cargo depressurization (0.72 atm equivalent), tropical sea-container humidity cycling (45°C / 85% RH), and vibrations per ISTA 3A. With minimum order quantities starting at 500 units and factory-direct pricing between $0.052 and $0.275, brands achieve Tier-1 multinational barrier reliability with zero middleman markups.
STAGE 05 · REAL-TIME BOM, CYLINDER FEE & MOQ ENGINE
Instant Pouch BOM, Cylinder Plate Fee & MOQ Calculator
Compare HP Indigo 25K Digital Print ($0 Cylinder Fee, MOQ 500–5,000) vs 10-Color High-Speed Rotogravure (MOQ 10,000+) in real time.
ENGINEERING & PROCUREMENT FAQ
Technical FAQ & Converting Troubleshooting
Q1: Does a Mono-PE pouch with an EVOH barrier layer still qualify as 100% recyclable in the EU and US?
Yes. Under both European RecyClass / CEFLEX guidelines (for EU PPWR 2026) and US APR / How2Recycle® standards, a polyethylene pouch containing less than 5.0% EVOH by total weight (our PM-EC-601 contains 3.8% EVOH and 96.2% PE) is certified fully compatible with the polyethylene recycling stream.
Q2: What is the realistic shelf life of an EN 13432 compostable pouch vs a Mono-PE recyclable pouch?
An EN 13432 compostable pouch (FSC Kraft / NatureFlex / PBAT+PLA) should be filled within 6 months of manufacture and provides a 9-to-12 month retail shelf life for dry goods stored below 28°C. If your product requires an 18-to-24 month shelf life or contains liquids/oils, we strongly recommend our Mono-PE (PM-EC-601) or GRS 35% PCR (PM-EC-604) structures.
RELATED BARRIER LAMINATE & POUCH SPECIFICATION CLUSTER (9-NODE TOPICAL MESH)
Related Pouch Structures, Converting SOPs & Direct Hub Directories
- Preventing Delamination in Acid & Oil Sachets
- EU PPWR 2026 Mono-Material PE Compliance Guide
- Home — Food & Cosmetic Pouches
- FDA / EU 10/2011 & Compatibility Lab
- Pillar 1: Food Stand-Up & Flat-Bottom Pouches
- Pillar 3: Cosmetic Sachets & Sheet Mask Pouches
- Pillar 5: High-Speed VFFS / HFFS Rollstock Film
- Laminate & Printing Comparison Hub
- Complete HTML Directory & Spec Index
STAGE 06 · 2-HOUR ENGINEERING DESK & 48H SAMPLE DISPATCH
Request Free 25-Pouch Sample Kit, 1:1 CAD Dieline & Factory-Direct FOB Quote
Only 3 required fields (*). Click any quick-spec capsule below or use the shortlist tray above. Alex Gao and our Guangzhou converting engineers respond within 2 business hours.